Textile Decoded
How a Spinning Mill Works
A plain walk through a ring spinning mill: blowroom, carding, combing, drawing, roving, ring frame and winding, and how polyester and viscose staple run on the same line as cotton.
Jump to section
- What a spinning mill does
- The line at a glance
- Blowroom: opening, cleaning and mixing
- Carding: the heart of the mill
- Combing: an optional step for finer cotton
- Drawing: doubling for evenness, and where blends meet
- Roving: the simplex frame
- Ring frame: where yarn is actually made
- Winding: clearing faults and building cones
- What this means for a fabric buyer
Quick answer
A spinning mill turns loose staple fiber into yarn in a fixed sequence. The blowroom opens and cleans the bales into small tufts. Carding separates the tufts into single fibers and forms a soft rope called sliver. Combing, for finer cotton yarns only, strips out short fibers. Drawing combines several slivers and stretches them into one even sliver. The roving (simplex) frame thins it and adds a light twist. The ring frame draws it down to the final count and twists it into yarn. Winding then removes faults and builds large cones for the weaver. Polyester and viscose staple go through the same machines, blended in at the blowroom or the draw frame.
What a spinning mill does
Fiber arrives at a spinning mill as dense, pressed bales: cotton lint from the gin, or polyester and viscose staple from the fiber plants. Inside a bale the fibers lie in tangled clumps, pointing in all directions, with some dust and, in cotton, leaf and seed fragments. Yarn needs the opposite: fibers lined up side by side, the same number of them in every centimetre, held together by twist.
Every machine in the mill does one of four jobs on the way there: open (pull the clumps apart), clean (take out trash and very short fibers), parallelise (line the fibers up) and attenuate (draw the strand thinner). Each stage hands a slightly thinner, more orderly strand to the next. This lesson follows ring spinning, the most common route for the fine, smooth yarn used in suiting and shirting. The next lesson compares it with open-end and air-jet spinning.
To be clear about where we sit: Benny Cotts does not spin yarn. We buy finished yarn from spinning mills and weave it in-house at our unit in Village Atoon, Bhilwara. This is a general explainer of how the industry makes the yarn every weaver depends on. If you have not read them yet, the Module 1 lessons on cotton from field to bale and polyester from crude oil to fiber explain where the fiber in those bales comes from.
The line at a glance
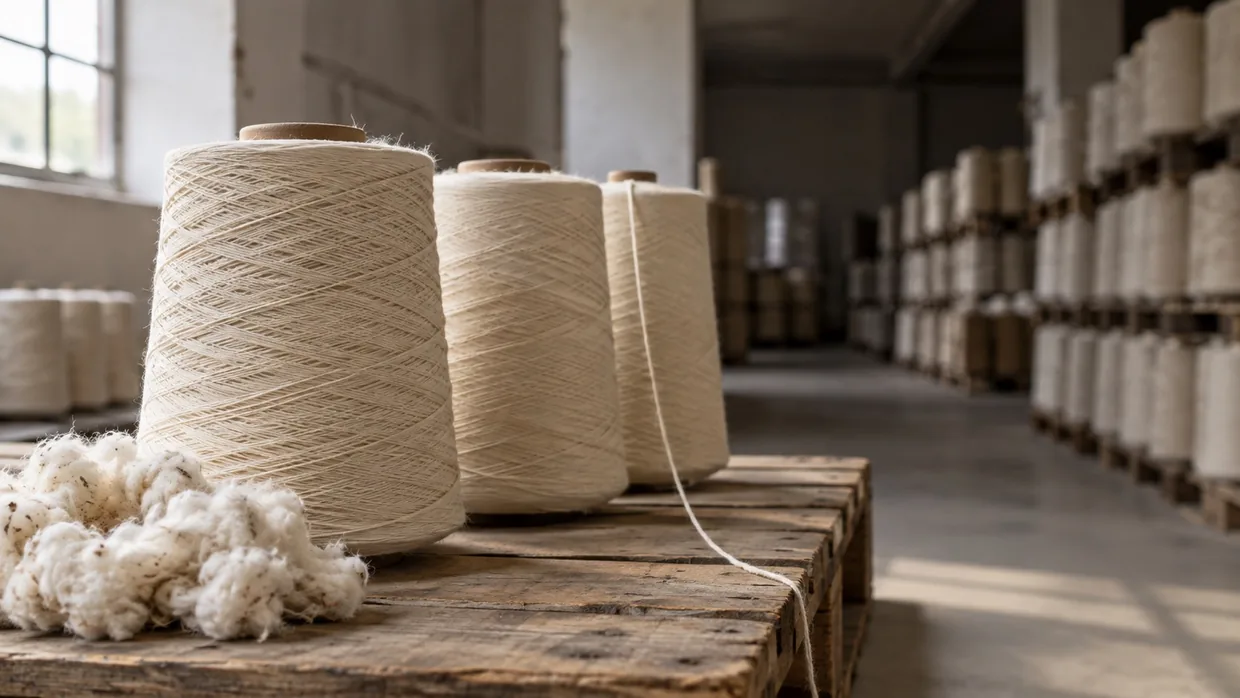
The sequence is the same in almost every short-staple ring spinning mill: blowroom, carding, combing (optional), drawing, roving, ring frame, winding. The names of the intermediate products change along the way. They are worth knowing because they come up in yarn specs and mill conversations. These are: tufts after the blowroom, sliver after carding and drawing, roving after the simplex frame, yarn on small bobbins called cops after the ring frame, and finally yarn on cones.
Short staple simply means fibers of cotton length, a few centimetres long. Polyester and viscose staple are cut to similar lengths precisely so that they can run on this same cotton-system machinery.
Blowroom: opening, cleaning and mixing
The blowroom is the first stage. An automatic bale plucker travels along a row of laid-down bales and picks small amounts off the top of each one in turn. Taking a little from many bales at once is the first act of mixing. It evens out the natural differences between cotton bales described in the cotton lesson.
The plucked fiber is carried by air through a series of opening and cleaning machines. Beaters and spiked rollers break the clumps into ever smaller tufts, and the heavier trash, such as leaf, seed coat and dust, falls out or is drawn away. Mixing machines then blend the tufts further before the material is fed to the cards.
Man-made staple is much simpler here. Polyester and viscose arrive clean, with no leaf or seed to remove, so they need opening rather than cleaning, and a mill tunes the blowroom to treat them gently.
Carding: the heart of the mill
Carding is often called the heart of spinning, because so much of the final yarn quality is decided here. The card has a large cylinder covered in fine wire teeth, working against other wire-covered surfaces. Tufts go in, and the wire teases them apart into single fibers, removes much of the remaining trash, and takes out many of the small fiber tangles called neps.
The fibers come off the card as a thin, cloudy web, which is gathered into a soft, untwisted rope about as thick as a thumb. This rope is called sliver, and it is coiled into tall cans. In card sliver the fibers are separated but still not well lined up, and many are hooked at the ends.
Yarn made from card sliver without combing is called carded yarn. Our guide to combed, carded and sanforized explains what that means for the feel and price of finished cloth.
Combing: an optional step for finer cotton
Combing is used only when the mill wants a finer, smoother, stronger cotton yarn. Several card slivers are first prepared into a lap, then the comber grips one fringe of fiber at a time and pulls fine needles through it. Short fibers, remaining neps and leftover trash are held back and removed as waste called noil.
How much noil is taken out is a deliberate choice that depends on the cotton and the target count. Published guidance from machine makers puts it very roughly between a tenth and a fifth of the material fed in, more for higher quality. Removing it costs fiber, which is why combed yarn costs more than carded yarn of the same count.
Polyester and viscose staple are normally not combed. They are cut to a uniform length at the fiber plant, so there are few short fibers to remove. In a combed poly-cotton yarn, it is the cotton that is combed, before it meets the polyester.
Drawing: doubling for evenness, and where blends meet
A single card or comber sliver is never perfectly even: it has slightly thick and thin stretches. The draw frame fixes this by doubling, feeding several slivers side by side (often six to eight) into one set of rollers. The thick places in one sliver tend to line up with thin places in another, so the combined strand is more even than any of its inputs.
The rollers then draft the strand: each pair of rollers turns faster than the pair before, so the fibers slide past each other and the strand is drawn out thinner. Drafting also straightens the fibers and lines them up along the sliver. Most mills pass sliver through two draw frame passages. Modern draw frames carry an autoleveller that measures the sliver and adjusts the draft to keep its weight steady.
The draw frame is also one of the two places where fibers are blended. In draw frame blending, polyester and cotton (or polyester and viscose) are carded separately. Their slivers are then fed together in the proportion needed, for example a set number of polyester slivers to cotton slivers. Repeated doubling over the passages mixes them thoroughly along the length. The other route is blending at the blowroom, where weighed tufts of each fiber are mixed before carding. This gives a closer fiber-to-fiber mix. Both are used in practice, and the choice depends on the fibers and the mill's setup. Our yarn counts and blends guide explains what blend ratios such as 65/35 mean for the cloth.
Roving: the simplex frame
Drawn sliver is still far too thick to spin directly into a fine yarn in one step. The roving frame, also called the simplex or speed frame, drafts it down to a much thinner strand called roving, roughly the thickness of a pencil lead or thinner.
Roving is so thin that it would fall apart if handled, so the simplex adds a small amount of twist, just enough to hold it together. This is called protective twist, and it is low enough that the next machine can still draft the strand. The roving is wound onto bobbins, which are then carried to the ring frame.
Ring frame: where yarn is actually made
The ring frame is where roving becomes yarn. Each spindle has its own drafting system, and here the roving is drawn out heavily to reach the final yarn count, the measure of how fine the yarn is.
As the thin strand leaves the drafting rollers, it is twisted. The yarn passes through a tiny clip called a traveller, which runs around a steel ring that surrounds a fast-spinning bobbin. The bobbin's spin, with the traveller lagging slightly behind it, puts twist into the yarn and winds it onto the bobbin at the same time. That twist is what turns a loose bundle of fibers into a strong yarn. More twist makes a harder, stronger yarn up to a point. Our glossary has a short entry on twist.
The full bobbins are called cops. Ring frames are slower and more labour-intensive than newer methods. But ring-spun yarn is strong, smooth and fine, which is why it remains the benchmark for quality suiting and shirting yarn.
Winding: clearing faults and building cones
A ring cop holds only a small amount of yarn, too little for a weaving mill. The automatic winder unwinds many cops and joins their yarn onto one large cone.
On the way, the yarn runs past an electronic yarn clearer, a sensor that checks it continuously. When it finds a fault, such as a thick place, a thin place or a bit of foreign fiber, the winder cuts it out and splices the two ends back together with air, so the join is nearly invisible and holds without a knot. This step catches many faults that would otherwise show up as defects in the woven fabric.
From here, cones may be sent out as single yarn or go on to be doubled and twisted into two-ply yarn, the ply often specified for suiting warps. They are then packed and shipped to weavers.
What this means for a fabric buyer
A buyer never sees a spinning mill, but its choices show up in the cloth. These choices all affect how smooth the fabric looks, how evenly it dyes and how well it resists pilling over time: combed or carded, the evenness achieved at the draw frame, how well blends were mixed, the twist set at the ring frame, and how strictly faults were cleared at winding. Our pilling guide explains one of those links.
This is why a weaver's yarn sourcing matters. We weave in-house at Village Atoon from yarn bought from spinning mills, and the cloth is then dyed and finished by partnered Bhilwara process houses.
Next lesson: Ring, open-end and air-jet spinning, three ways to make the final yarn and why they feel different in cloth. Browse the full course on the Textile Decoded hub.
FAQ
Frequently asked questions
- What is the difference between sliver, roving and yarn?
- Sliver is the soft, untwisted rope of fiber that comes off the card and draw frame. Roving is a much thinner strand made from sliver on the simplex frame, with a little twist to hold it together. Yarn is the final product of the ring frame: drafted to its count and fully twisted.
- Why is combing optional?
- Combing removes short fibers and neps to make finer, smoother, stronger cotton yarn, but it discards a share of the fiber as noil and adds a process step. Coarser yarns do not need it, and polyester and viscose staple are cut to uniform length, so they are normally not combed.
- Where are polyester and viscose blended in a spinning mill?
- In one of two places. At the blowroom, weighed tufts of each fiber are mixed before carding. At the draw frame, each fiber is carded separately and the slivers are combined in the right proportion, with repeated doubling mixing them along the length. Both routes are in common use.
- Why does yarn go through winding after the ring frame?
- Ring frame bobbins (cops) hold too little yarn for weaving. Winding joins many cops onto one large cone and, on the way, an electronic clearer cuts out thick, thin and contaminated places and splices the ends together.
- Does Benny Cotts spin its own yarn?
- No. We buy yarn from spinning mills and weave it in-house at our unit in Village Atoon, Bhilwara. Dyeing and finishing are done by partnered Bhilwara process houses. You can Request Catalog at /quote to see the fabrics we weave.
Cite this guide
Quoting this page? Paste the line below so the credit links back.
<a href="https://www.bennycotts.com/guides/how-a-spinning-mill-works">How a Spinning Mill Works</a>, Benny Cotts, 2026Next in Yarn
Ring, Open-End and Air-Jet Spinning Explained
More in Yarn
- How a Spinning Mill Works
- Ring, Open-End and Air-Jet Spinning Explained
- Yarn Counts and Blends Explained
- Combed, Carded, Sanforized: Spec-Sheet Terms Explained
- Texturised Yarn in Suiting: What It Is and What It Changes
- What Moves Yarn Prices: Fiber, Count, Spinning and the Market
- Yarn Quality: What to Check Before It Becomes Fabric
Updated 15 October 2026 · Benny Cotts, Bhilwara
Fabrics
Fabrics mentioned in this guide
Spec, price and MOQ on every fabric page.

Nano
Poly-Viscose blend · 180-200 GSM
Our entry-level uniform fabric for large-volume programs.

Sonata
Poly-Viscose blend · 190-210 GSM
Cost-efficient uniform fabric without compromising weave quality.

Grado 1st
Poly-Viscose blend · 220-240 GSM
Tailoring-grade fabric built for everyday durability.
Industries this applies to
Uniform programs these fabrics are used for
- Fabric for Business Attire
- Fabric for Corporate Uniforms
- Fabric for Corporate Shirts
- Fabric for Corporate Trousers
- Fabric for Blazers & Waistcoats
- Fabric for School Uniforms
- Fabric for College & University Uniforms
- Fabric for Sports & PT Uniforms
- Fabric for Pre-School & Kindergarten Uniforms
- Fabric for Doctor Coats
- Fabric for Nurse Scrubs
- Fabric for Lab Coats
- Fabric for OT & Surgical Wear
- Fabric for Patient Gowns
- Fabric for Hospital Staff Uniforms
- Fabric for Chef Coats
- Fabric for Salon & Spa Uniforms
- Fabric for Cabin Crew Uniforms
- Fabric for Ground Staff Uniforms
- Fabric for Army Uniforms
- Fabric for Police Uniforms
- Fabric for Security Guard Uniforms
- Fabric for Industrial Uniforms
- Fabric for Construction Workwear
- Fabric for Housekeeping Uniforms
- Fabric for Business Suits
- Fabric for Black-Tie Attire
- Fabric for Formal Event Wear
Fabric types covered here
Keep reading
Related guides
Ready to place an enquiry?