Textile Decoded
Cotton: From Field to Bale
How cotton is sown, grown, picked, ginned and baled in India, and what staple length and micronaire tell a spinner about the fiber before it ever becomes yarn.

Jump to section
Quick answer
Cotton is the seed hair of a shrub. In India it is mostly sown with the monsoon, picked by hand from the open bolls in several rounds, and taken to a gin, where the fiber (lint) is pulled off the seed. Lint is roughly a third of the picked weight. It is pressed into bales and sold to spinning mills, which judge it on staple length (how long each fiber is), micronaire (fineness and maturity), strength and cleanliness. These decide how fine and even a yarn the cotton can make.
What cotton actually is
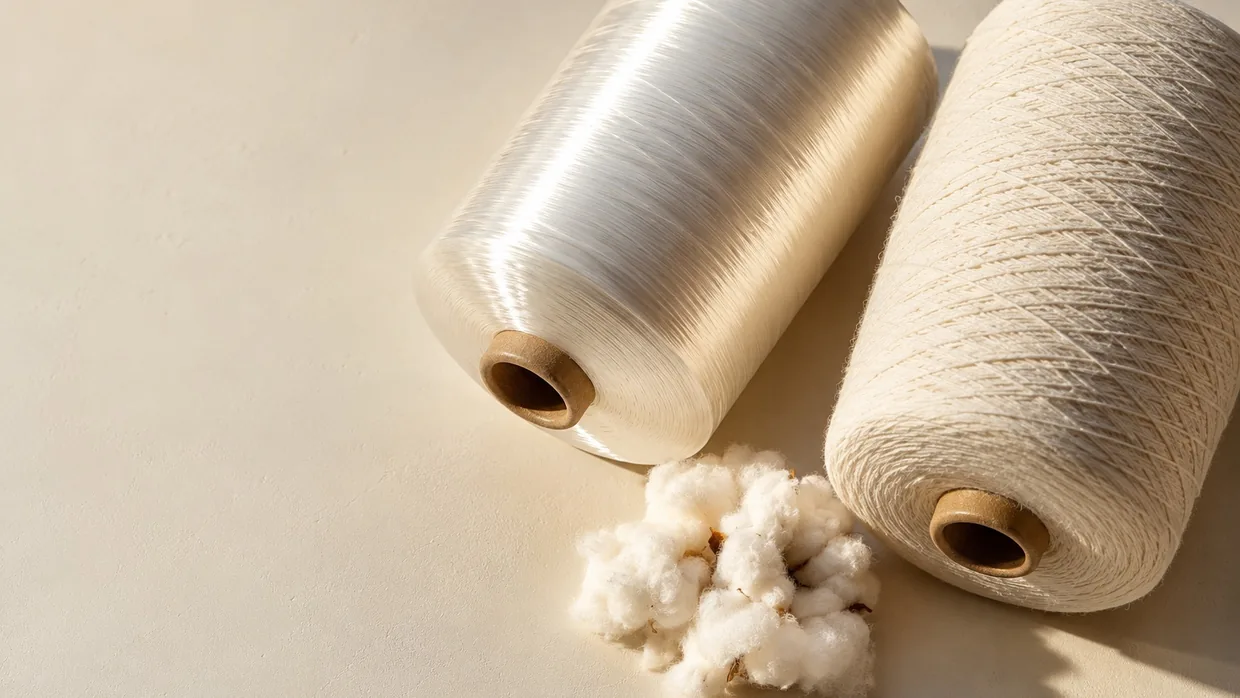
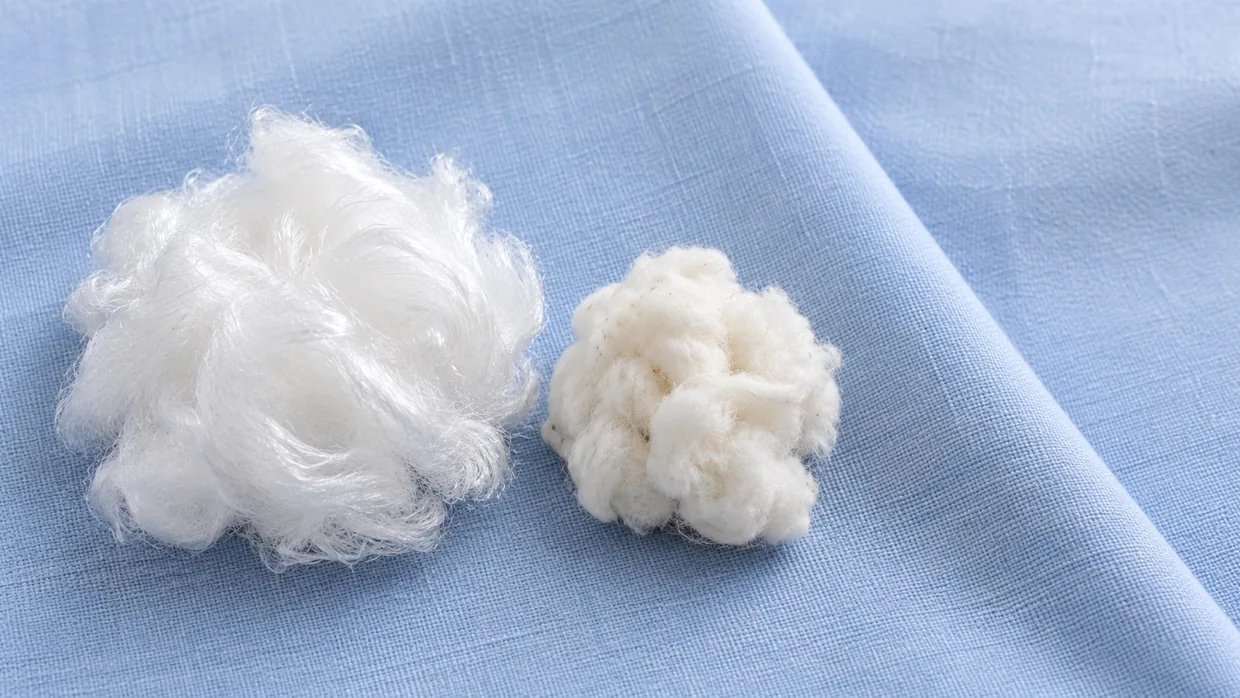
Cotton is a natural fiber: it grows, rather than being made in a factory. Each fiber is a single long plant cell that grows out of the surface of a cottonseed inside a pod called a boll. When the boll ripens and splits open, the fluffy white mass you see is thousands of these fibers still attached to their seeds. The fiber is almost pure cellulose, the same material that makes up wood and paper, which is why cotton absorbs water, breathes well and takes reactive dyes.
Because cotton is a crop, every lot is a little different. Weather, soil, seed variety and how it was picked all leave a mark on the fiber. This natural variation is a key idea in this lesson. It is the main reason mills test cotton before buying it. If you are new to the fiber families, the previous lesson on natural, man-made and synthetic fibers shows where cotton sits next to polyester and viscose.
Sowing and the monsoon
In India cotton is a kharif crop, meaning it is sown at the start of the rainy season and harvested after it. In the north, where most cotton land is irrigated, sowing starts earlier, from around April and May. Across the central and southern belt much of the crop is rain-fed, so farmers wait for the monsoon to arrive before they sow, usually in June and July.
This is why the monsoon matters so much to cotton. A late or patchy monsoon delays sowing, can push farmers toward other crops, and stresses the plants while they flower and set bolls. Too much rain at picking time causes problems as well, because wet open bolls discolour and the fiber can be damaged. For these reasons, traders watch sowing area and rainfall reports closely. A later lesson in this module covers how those signals move fiber prices.
India's cotton belt
Cotton is grown across three broad zones. The northern zone (Punjab, Haryana and Rajasthan) is mostly irrigated. The central zone (Gujarat, Maharashtra and Madhya Pradesh) is the largest by area and much of it is rain-fed. The southern zone (Telangana, Andhra Pradesh, Karnataka and Tamil Nadu) completes the belt, with Odisha also growing a smaller crop.
The Indian cotton season is counted from October to September, because that is when new-crop cotton starts reaching the market. Crop size is reported in bales of 170 kg of lint each, so a figure quoted in lakh bales is a count of that unit. Rajasthan, home to the Bhilwara textile cluster, is one of the growing states. But a mill's yarn can be spun from cotton grown anywhere in the country. Our guide on why Bhilwara is a textile hub covers the cluster itself.
Picking and ginning: from kapas to lint
Bolls on the same plant do not all open at once, so Indian cotton is mostly picked by hand in several rounds over a few months, from around October into the new year. What comes off the plant is seed cotton, known in India as kapas: fiber and seed still joined together, plus some leaf and dirt. Hand picking is gentle on the fiber. But loose bits of cloth, hair or plastic can get mixed into the kapas. This is called contamination, and it is a real quality problem later, because these bits cannot be removed once the cotton is spun into yarn.
Kapas goes to a ginning factory. Ginning is the step that separates the fiber from the seed. Two kinds of gin are common. Roller gins pull the fiber off between a roller and a fixed blade and are gentle on longer fibers. Saw gins use rows of toothed discs and are faster. Either way, the gin produces two products from one crop. The lint is the fiber that goes on to spinning, and it is roughly a third of the seed cotton by weight. The cottonseed is the larger share. It is crushed for oil and cattle feed, and the short fuzz left on it after ginning, called linter, is sold separately as a raw material for other industries.
Bales: how cotton travels
After ginning, the lint is cleaned and pressed under heavy pressure into a dense block, wrapped and strapped. That block is a bale. In India a bale holds 170 kg of lint. Pressing makes cotton practical to store and ship, and each bale carries a lot identity so that a spinning mill can trace and test what it bought.
Spinning mills buy cotton by the bale and blend lint from many bales together before spinning. That blending, called bale mixing, evens out the small differences from bale to bale so the yarn stays consistent from one day to the next. It is the first of many steps between field and fabric that exist to manage cotton's natural variation.
Staple length and micronaire: what spinners measure
Staple length is the length of the individual fibers. Longer fibers overlap more along the yarn, so a spinner can make a finer, smoother and stronger yarn with fewer loose fiber ends sticking out. Short staple suits coarser yarns. Most shirting and uniform cotton is spun from medium to long staple. Extra-long staple (ELS), above about 34 mm, is reserved for very fine counts. Staple length also affects how a fabric wears: shorter fibers work loose more easily, which is one cause of the fuzz balls covered in our pilling guide.
Micronaire is a measure taken by blowing air through a weighed plug of fiber. The reading reflects how fine and how mature the fibers are together. Too low usually means immature fiber, which can form tangles called neps and dye unevenly. Too high usually means coarse fiber, which limits how fine a yarn can be spun. Mills also test fiber strength, uniformity, colour grade and trash content, mostly on high-volume testing instruments. Then they decide which bales go into which yarn.
Fiber quality is only the start. How the yarn is then spun, whether it is combed to remove short fibers, and its count all shape the finished cloth, as explained in combed, carded and sanforized and our yarn counts guide.
Organic and Better Cotton, briefly
Two terms come up often. Organic cotton is grown without synthetic fertilisers or pesticides and from non-genetically modified seed. The claim has to be backed by certification of the farm and of every later stage that handles the fiber. Better Cotton, the programme formerly known as BCI, is a separate scheme that trains farmers in more efficient water and pesticide use. It is not organic. Much Better Cotton is tracked through a mass-balance system, which means the volume is accounted for rather than kept physically separate.
Both are claims about the fiber and its chain of custody (the record of who handled it at each stage), not something you can see in the cloth. A buyer who needs either should ask for the relevant documents at each stage. Our guide to sustainability certifications explains what each scheme covers and what paperwork to expect.
Where this leads
From the bale, cotton goes to a spinning mill to become yarn, and then to a weaver. We do not grow cotton or spin yarn. We weave in-house at our unit in Village Atoon, Bhilwara, from yarn bought from spinners. Our cotton-blend cloth, such as the poly-cotton Cambery chambray, carries cotton's breathable, matte character into uniform shirting. For how cotton compares with blends in daily wear, see poly-viscose vs cotton uniforms.
Next in Module 1: Polyester, from crude oil to chip to fiber, the man-made half of most uniform blends. Browse the full course on the Textile Decoded hub.
FAQ
Frequently asked questions
- What is the difference between kapas and lint?
- Kapas is seed cotton as it is picked: fiber still attached to the seed. Lint is the fiber after ginning has removed the seed. Lint is what is baled and sold to spinning mills, and it is roughly a third of the kapas by weight.
- Why does the monsoon affect cotton supply?
- Much of India's central and southern cotton is rain-fed, so sowing waits for the monsoon. A late or weak monsoon delays sowing and stresses the crop, while heavy rain at picking time can damage open bolls. Both can reduce the quantity or quality of the crop that reaches the market.
- Is longer staple cotton always better?
- Not always. Longer staple allows finer, smoother yarn, which matters for fine shirting. For a medium count uniform yarn, medium to long staple with good strength and micronaire within the normal range is the sensible choice. Paying for extra-long staple adds little.
- How much does an Indian cotton bale weigh?
- An Indian bale holds 170 kg of lint. Bales in some other markets are heavier, so crop figures from different countries are not directly comparable without converting the unit.
- Does Benny Cotts sell organic or Better Cotton fabric?
- We do not hold organic or Better Cotton certification, so we do not make those claims for our cloth. If a programme needs a certified fiber chain, tell us at enquiry stage and we will be clear about what can and cannot be documented. You can Request Catalog at /quote to see what we stock.
Cite this guide
Quoting this page? Paste the line below so the credit links back.
<a href="https://www.bennycotts.com/guides/cotton-from-field-to-bale">Cotton: From Field to Bale</a>, Benny Cotts, 2026Next in Fibers
Polyester: From Crude Oil to Fiber
More in Fibers
- What Is a Fiber? Natural, Man-Made and Synthetic
- Cotton: From Field to Bale
- Polyester: From Crude Oil to Fiber
- Viscose: Fiber From Wood Pulp
- Wool, Linen, Nylon and Elastane: The Rest of the Fiber Family
- What Moves Fiber Prices: Cotton, Polyester and Viscose
- Blends Compared: Poly-Viscose, Poly-Cotton, Cotton and Polyester
- Poly-Viscose vs Cotton for Uniforms: 7 Differences
- Poly-Viscose and Poly-Cotton Ratios Explained: The Manufacturing Reasons Behind Each Blend
- Why 65/35 Is a Common Ratio for Uniform Shirting
- 100% Polyester Suiting for Uniforms: Where It Wins and Where It Loses
- Stretch and Lycra Uniform Fabric, Explained
Updated 12 October 2026 · Benny Cotts, Bhilwara
Fabrics
Fabrics mentioned in this guide
Spec, price and MOQ on every fabric page.


Industries this applies to
Fabric types covered here
Keep reading
Related guides


Ready to place an enquiry?